Burner India: Biomass, Dual-Fuel & IoT Burners for Asphalt Plants

Vinesh Bhatia
Burner India

We combine fuel flexibility, combustion efficiency and application-specific solutions to meet the evolving demands of industrial heating, with our CE-certified products enabling us to serve international export markets.

Vinesh Bhatia
Director
Burner India’s portfolio includes dual-fuel burners, IoT-based burners, and thermic fluid heaters with multiple fuel options. Our biomass-based and IoT-enabled burner technologies help industries cut fuel costs, lower emissions, and achieve more efficient heating operations. Our dual-fuel burners, IoT-based burners, and thermic fluid heaters come with multiple fuel options. Our asphalt batch mix plant burners and biomass burners deliver high efficiency and versatility across industrial heating needs.

We offer a comprehensive range of solutions.
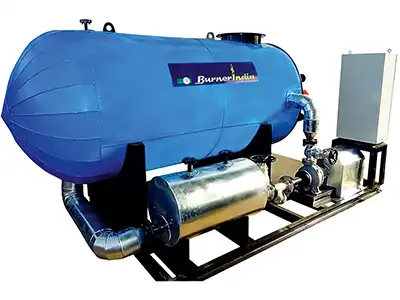
burner India
Burner India’s range also features Step Less Modulation Systems using technology from Siemens, Honeywell, Lamtec, and Autoflame, equipped with PLCs that automatically regulate O2, CO, CO2, NOx, and SOx levels for precise temperature control. These systems automatically adjust oxygen levels to achieve optimal combustion.

Our Mono Block modulating burners, available with aluminium or steel casings and integrated or separate electrical switch cabinets, feature adjustable combustion heads for various chamber designs and a PID system controller with digital set points and real-time performance displays.
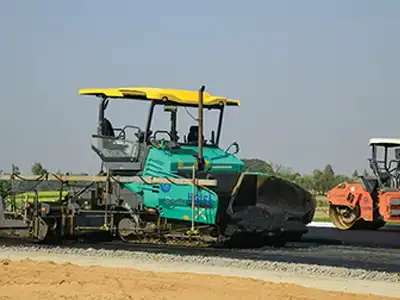
We have developed biomass-based burners that cut 25–60% fuel costs.

To meet the industry’s demand for lower operating costs and sustainable energy use, we introduced biomass burners in 2013. Running on wood pellets, these burners are used for heating thermic fluid and bitumen in asphalt batch mix plants, offering 25–60% cost savings over diesel or LDO while reducing carbon footprints. Our biomass systems use carbon-neutral fuels and ensure complete combustion through optimized air-to-fuel ratios, supporting fuels like FO, LDO, HSD, biodiesel, LPG, PNG, and biogas.

IoT and digital components in our products are transforming burner control and user convenience.

As part of our continuous innovation, Burner India has been incorporating IoT and digital components into our products. This shift towards smart technology allows users to remotely control and monitor burner operations from anywhere. Operators can access data sheets and performance analytics directly from their smartphones, enabling real-time insights, easier maintenance, and greater convenience in managing operations.

CE certifications have allowed us to supply to European markets.

We uphold strict quality, safety, and customization standards in manufacturing. As an ISO 9001-certified company, we follow rigorous in-house manufacturing, testing, and quality assurance procedures, including inward material checks, quality tests, and performance evaluations. Our CE certifications enable us to supply to European markets, ensuring compliance with global safety norms. Every burner is fully customizable to meet specific client requirements, delivering consistent performance, efficiency, and reliability across applications.